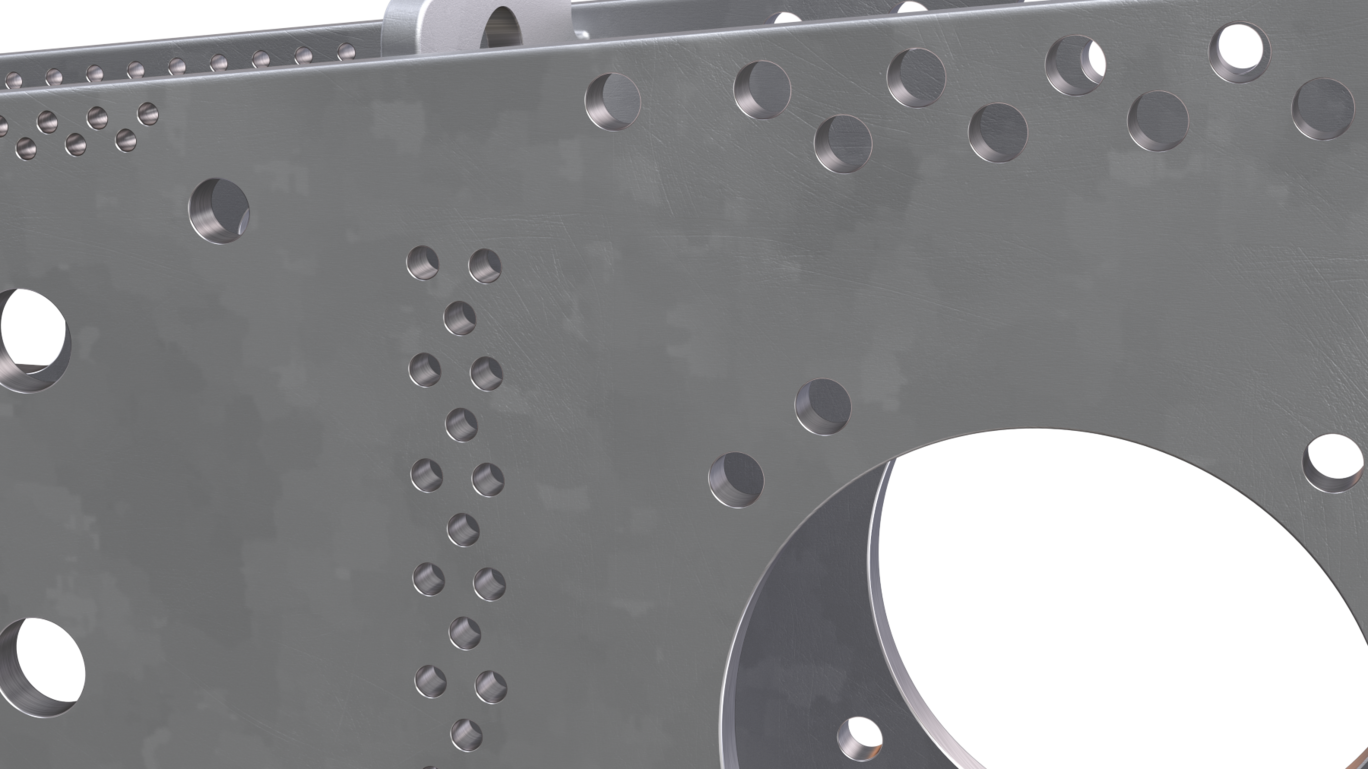
Pylon
Automatic forward and reverse chamfering of bores in pylons
The pylon anchors the turbine to the aircraft wing and absorbs all the thrust forces. The pylon contains all the mechanical and electrical interfaces. The quality requirements are correspondingly high.
The numerous bores are only drilled once the pylon has been pre-assembled. This is carried out simultaneously from both sides on a twin-spindle machine. The plates, which consist of two different materials (layered structure), present a further challenge.
| Workpiece | Pylon |
| Material | Titanium, 15-5 PH steel (layered structure) |
| Drill diameter | 8.0 mm |
| Chamfer diameter (forward) | 8.4 mm |
| Chamfer diameter, reverse | 9.8 mm |

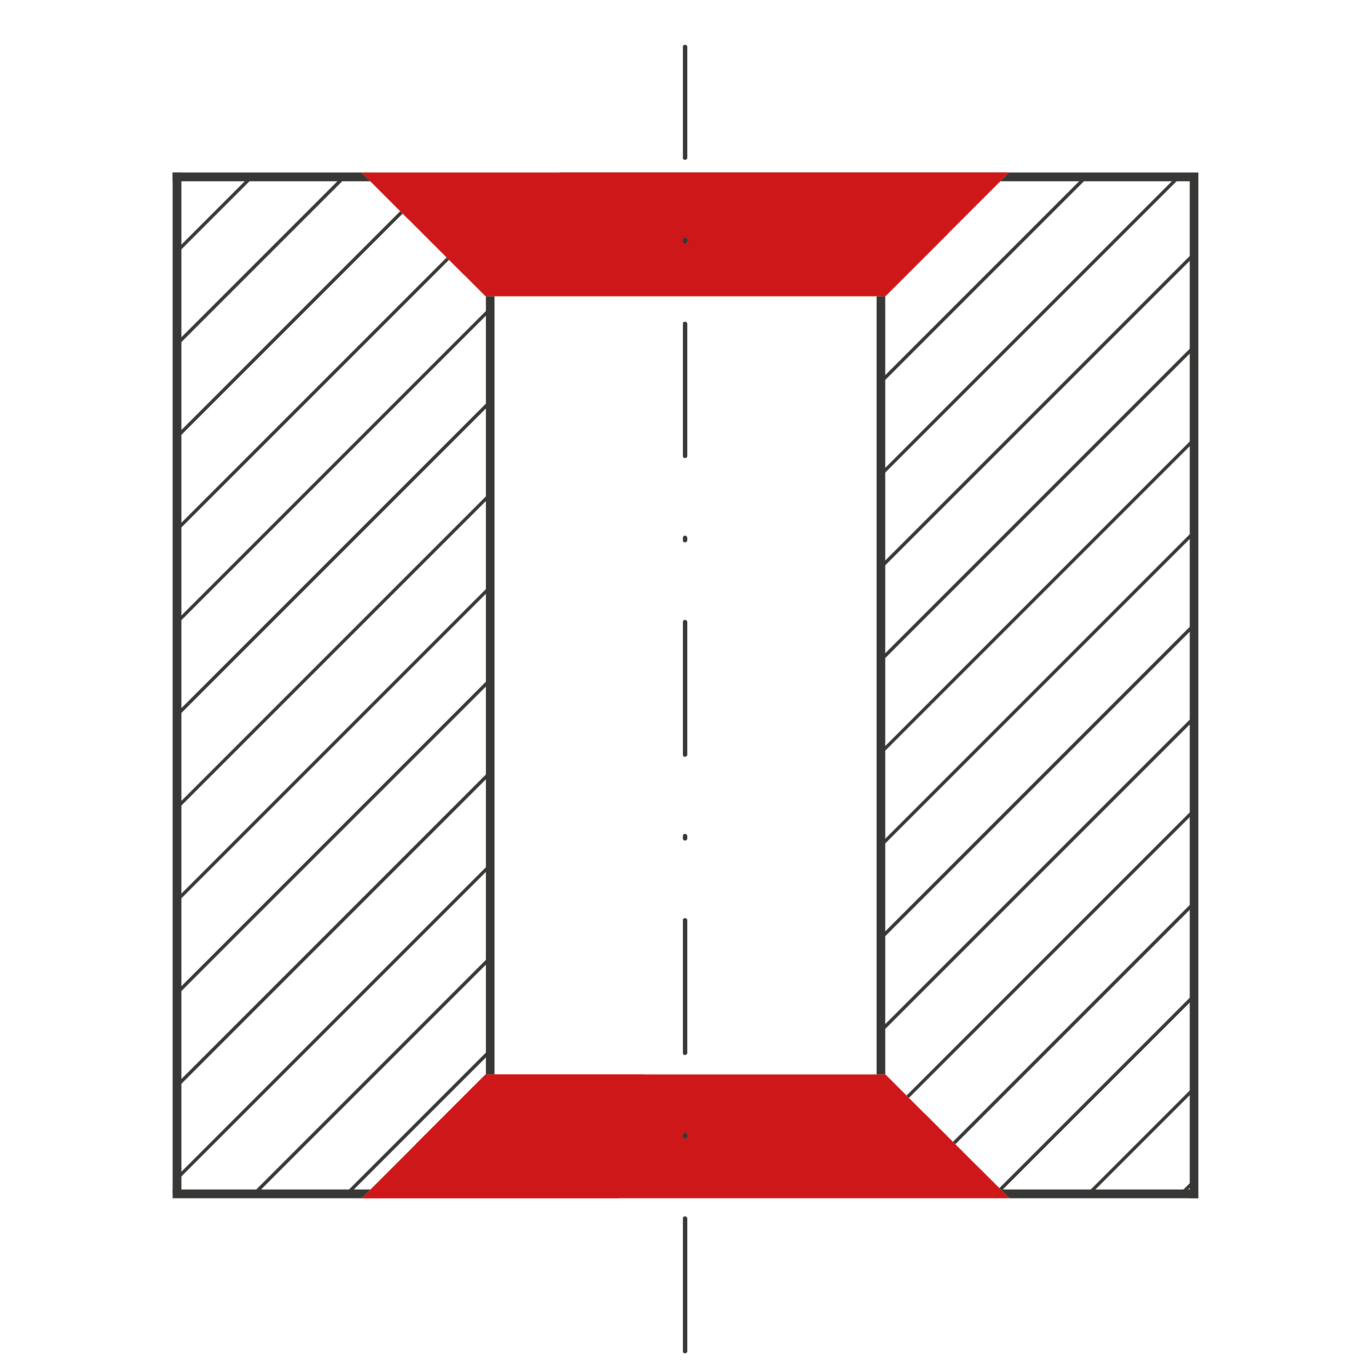
As these are blind bores, it is essential that the chamfers are machined to a high standard. To ensure the chamfers on the numerous bores are machined to a high standard, a tool system was required that could handle different diameters and materials, and machine in both forward and reverse directions. With the DEFA deburring tool, the component is machined from both sides simultaneously, thereby meeting all the specified requirements.